
Temperature Control in Die Casting: Why Die Temperature and Cooling Matter
Every casting cycle introduces a considerable amount of heat into the die. This energy must be managed in a controlled way: enough heat has to be removed to support solidification and stable cycle times, while the die must remain within the temperature range required for reliable mold filling. Water- and thermal-oil-based temperature control systems are therefore an important part of modern die casting cells.
Why Is Die Temperature Control Important?
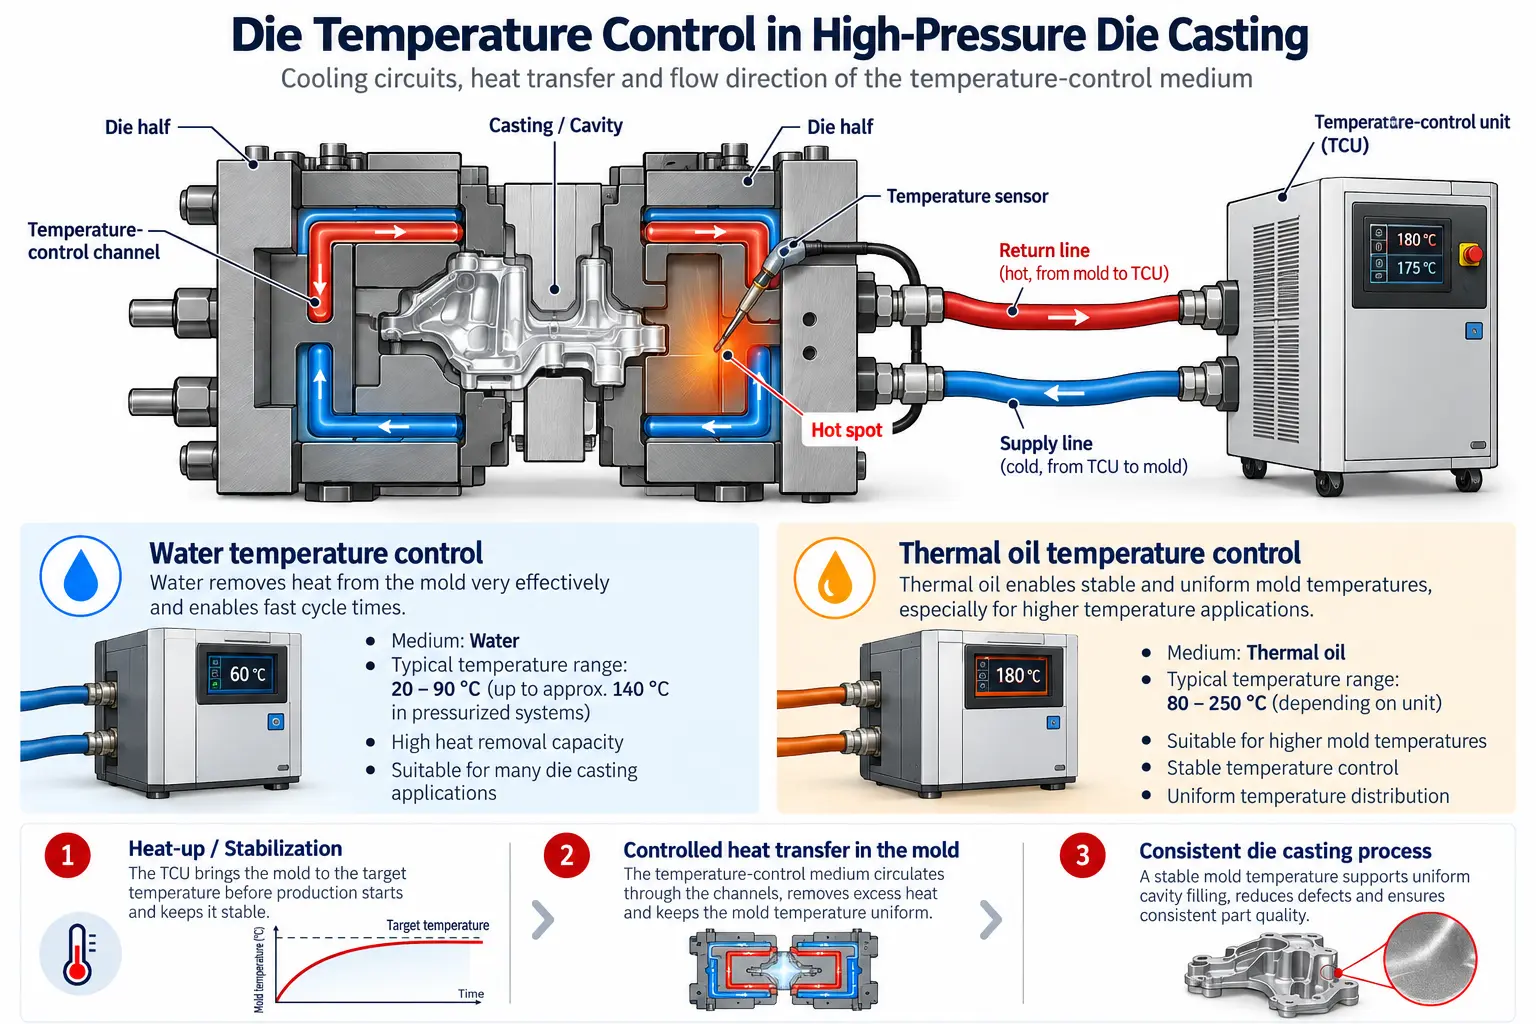
A temperature control unit circulates a heat-transfer medium through channels inside the die. Depending on the operating condition, the system can bring heat into the tooling or remove excess process heat.
The objective is not maximum cooling. The objective is a repeatable thermal balance in which die temperature, mold filling, solidification and cycle time remain as stable as possible from shot to shot.
The Die Absorbs Heat During Every Casting Cycle
When molten metal enters the closed die, heat is transferred from the metal into the die surface and the surrounding tooling. The casting begins to solidify while the temperature of the affected die areas rises.
After the casting is removed, the next cycle introduces heat again. At the same time, energy is removed through the die, temperature-control circuits, spraying process, machine structure and surrounding environment.
A stable series process therefore requires a thermal condition that becomes repeatable over successive casting cycles. This does not mean that every part of the die has the same temperature. Cores, inserts and areas close to heavy sections of the casting can experience very different thermal loads.
How the Temperature-Control Circuit Works
The temperature-control unit and the die form a closed thermal circuit. A pump moves the temperature-control medium through hoses and internal die channels.
The supply and return conditions depend on whether the system is currently heating, stabilizing or removing process heat. The important point is that the medium circulates continuously through the defined circuit and transports thermal energy between the temperature control unit and the die.

Heating, Stabilizing and Removing Heat
Bring the Die to Operating Temperature
Before stable series production begins, the tooling must reach an appropriate thermal condition. Starting with a die that is too cold changes the thermal conditions during the first casting cycles.
Maintain Repeatable Thermal Conditions
During production, the thermal state should not continue to drift from shot to shot. The temperature-control system helps maintain a repeatable operating range.
Control Thermally Loaded Areas
Areas exposed to high local heat input may require more intensive temperature control than less heavily loaded areas of the die.
Both Excessively Cold and Excessively Hot Areas Can Affect the Process
Molten metal must travel through the gating system and fill the cavity before excessive local solidification takes place. If parts of the die are too cold, heat can be extracted from the melt particularly quickly and the available mold-filling time may be reduced.
If areas remain too hot, local solidification and cooling can take longer. This can influence the time required before the casting can be removed from the tooling.
The goal is therefore not one universally low die temperature. What matters is a controlled temperature distribution that matches the casting, alloy, die design and production cycle.
| Condition | Possible Effect | Temperature-Control Objective |
|---|---|---|
| Die area too cold | Rapid heat extraction and changed mold-filling conditions. | Maintain critical areas within the intended operating range. |
| Die area too hot | Slower local solidification and cooling. | Remove excess process heat in a controlled manner. |
| Uneven temperature distribution | Different solidification conditions within the same casting. | Improve the repeatability of local thermal conditions. |
| Temperature drifts over time | Casting conditions change despite unchanged machine settings. | Establish a stable cyclic thermal balance. |
Cooling Performance Depends on the Complete Circuit
Temperature-control channels are positioned inside the die to transfer heat between the tooling and the circulating medium. Their effectiveness depends on more than simply having a large channel diameter.
Channel position relative to the cavity, cross-section, circuit length, heat-transfer conditions, flow rate and pressure loss all influence the actual thermal performance.
Complex dies can therefore contain several separate circuits. This makes it possible to manage thermally different areas, such as cores, inserts or locally highly loaded sections, more independently.
Water or Thermal Oil: Which Medium Is Used in Die Casting?
Water and thermal oil are both used as heat-transfer media in die casting temperature-control systems. They perform the same fundamental task: transporting thermal energy between the temperature control unit and the die.
They are not interchangeable in every application. Temperature range, system pressure, heat-transfer behavior, pump design, seals, hoses and die circuits must all be compatible with the selected medium.
High Heat Transfer and Fast Thermal Response
Water provides effective heat transfer and is therefore well suited to many die casting temperature-control and cooling applications.
For applications above the normal atmospheric boiling range, closed pressurized-water systems can be used. Operating pressure, water quality, corrosion protection, deposits and the pressure rating of the entire circuit must then be considered.
Temperature Control at Higher Operating Temperatures
Thermal-oil units are commonly used where higher supply temperatures are required or where the process is designed around an oil-based high-temperature circuit.
The condition of the thermal oil, pumps, heaters, seals, expansion system and cooling concept becomes particularly important at elevated operating temperatures.
Why Hot Spots Develop Inside a Die Casting Die
A die casting rarely has the same wall thickness throughout. Larger material accumulations or locally unfavorable heat-transfer conditions can introduce more heat into certain die areas than surrounding regions.
These areas can remain thermally loaded for longer periods and affect local solidification behavior. A reasonable average die temperature therefore does not automatically mean that all critical areas are thermally balanced.
Temperature sensors, thermal imaging and casting-process simulation can help identify such differences. The information can then be used to optimize channel layout, operating conditions or individual temperature-control circuits.
What Does a Temperature Control Unit Actually Do?
A temperature control unit circulates the selected medium through one or more circuits and controls its thermal condition. Depending on the process state, the system can heat the tooling, remove heat or keep the temperature within the required range.
For technical selection, the maximum temperature alone is not enough. Heating capacity, cooling capacity, pump performance, flow rate, operating pressure and number of circuits must also match the actual tooling.
FISS offers used water and thermal-oil temperature control units, including single- and multi-circuit systems as well as pressurized-water and mobile cooling solutions.
Available equipment can be found in the FISS section for used temperature control units .
How the Thermal Condition Changes During Production
Bring the Die to Operating Temperature
Before stable production begins, the die is brought into the intended thermal operating range.
Introduce Molten Metal
Molten metal enters the die and rapidly transfers thermal energy to the tooling.
Solidification Begins
Heat flows from the casting into the die while the casting solidifies and continues to cool.
Transfer Heat Through the Temperature-Control Circuit
The circulating medium transports thermal energy between the die and temperature control unit.
Open the Die and Remove the Casting
Once sufficient solidification has occurred, the die opens and the casting is removed.
Repeat Under Stable Thermal Conditions
During series production, the goal is a repeatable thermal state from one cycle to the next.
Internal Circuits Are Only One Part of the Thermal System
The internal temperature-control circuit is not the only factor affecting die temperature. Die spraying and air blowing also change the thermal condition of the exposed die surface between casting cycles.
Spray duration, release-agent quantity, air flow and cycle time therefore interact with internal temperature control. A thermal problem should not automatically be compensated for only by increasing spray cooling.
In an automated casting cell, die temperature control, spraying, casting machine and handling equipment should therefore be considered as parts of the same production process.
More information about the complete cell is available in Automation in the Die Casting Cell .
What Should Be Checked When Selecting a Temperature Control Unit?
Especially with used equipment, the nameplate temperature is only one part of the technical assessment. The complete hydraulic and thermal system must match the new application.
- temperature-control medium: water or thermal oil
- required supply and return temperatures
- heating capacity
- cooling capacity
- number of temperature-control circuits
- required flow rate per circuit
- pump performance and operating pressure
- pressure loss through die channels, hoses and couplings
- die size, mass and thermal load
- hose and connection dimensions
- temperature sensors and monitoring
- control system and machine interfaces
- condition of pumps, heaters, valves and heat exchanger
- maintenance history and available documentation
Temperature Control Cannot Be Optimized in Isolation
Die temperature interacts with molten-metal temperature, mold filling, solidification, spraying and cycle time. Changing one parameter can therefore influence several other stages of the process.
This applies to both cold-chamber and hot-chamber die casting. The method used to supply molten metal differs, but both processes rely on controlled thermal conditions inside the permanent die.
The differences between the two machine concepts are explained in Cold Chamber or Hot Chamber? .
Stable Die Casting Requires a Stable Thermal Balance
During every casting cycle, thermal energy moves from the molten metal into the die and must subsequently be controlled. Temperature control units provide the circulation and thermal management required to keep this process repeatable.
Water offers effective heat transfer and is widely used for cooling and temperature-control applications. Thermal oil provides an alternative for systems designed for higher operating temperatures.
The correct solution depends not only on the medium, but also on die channels, flow rate, pressure, heating and cooling capacity, tooling design and cycle conditions. These factors should always be evaluated as one complete system.
Questions About Temperature Control in Die Casting
Why Does a Die Casting Die Need Temperature Control?
Molten metal introduces heat into the die during every casting cycle. Temperature control helps maintain a repeatable thermal state by transferring heat between the die and the temperature control unit.
Is Temperature Control the Same as Cooling?
No. The tooling may first need to be heated to its intended operating condition. During production, the system can then remove excess heat or stabilize the die temperature.
Is Water or Thermal Oil Better for Die Casting?
Neither medium is universally better. Water provides very effective heat transfer, while thermal oil is commonly used for higher-temperature applications. The correct choice depends on the required temperature range and the design of the entire circuit.
Can Water Be Used Above 100 °C?
Yes. Closed pressurized-water temperature-control systems can operate above the atmospheric boiling point of water. The complete circuit must be designed for the corresponding operating pressure and temperature.
What Is a Hot Spot in a Die Casting Die?
A hot spot is an area of locally elevated thermal load. It can develop where more heat enters the tooling than is removed during the available cycle time.
Why Is Flow Rate Important?
The heat-transfer medium must actually circulate through the die channels at the required rate. Pump performance, pressure losses, hoses, couplings and channel geometry all influence the achievable flow.
Can a Used Temperature Control Unit Be Installed on Another Die Casting Machine?
Potentially, yes. However, medium, temperature range, heating and cooling capacity, pump performance, flow rate, operating pressure, number of circuits and connections must match the new die and production process.
FISS Offers Used Water and Thermal-Oil Temperature Control Units for Die Casting.
The right unit must match the thermal requirements of the die as well as the medium, flow rate, pump performance, heating and cooling capacity and existing temperature-control circuits.
Source
Bührig-Polaczek, A.; Michaeli, W.; Spur, G. (eds.): Handbuch Urformen, Carl Hanser Verlag. In particular, the fundamentals of permanent molds, heating and cooling systems, thermal balance and die casting were considered.